ERP and MES are both important parts of a modern manufacturing environment, but they serve very different purposes. This ERP vs MES guide explains how the two systems differ, how they work together, and why an ERP system alone does not always provide the shop-floor visibility manufacturers need.
The article looks at the role of MES in manufacturing operations and how it connects production plans with what is happening on the factory floor. Most importantly, the article explains that ERP and MES are not competing systems. ERP manages the business and production plan, while MES focuses on executing that plan and providing visibility into what is happening on the shop floor.
Navigate to section

- 1. What is ERP (Enterprise Resource Planning)?
- 2. What is MES (Manufacturing Execution System)?
- 3. Key Functionalities and Benefits of MES
- 4. MES vs ERP: What is the Difference Between MES and ERP?
- 5. How Does ERP Create a Manufacturing Gap?
- 6. ERP and MES Integration: How They Work Alongside
- 7. MES vs ERP: The Difference in Practice
The manufacturing ecosystem is flooded with advanced technologies and software that improve efficiency and overall output. ERP and MES are two of those advanced tools that simplify manufacturing challenges in many ways.
ERP vs MES: Quick Overview
ERP plans and pays for what your business makes; it is built to run and manage the business data. MES (Manufacturing Execution System) tracks, monitors, and controls the process execution in real time; it is built to run a factory efficiently.
ERP and Manufacturing Execution System are often mentioned together, but they’re not the same thing, and one doesn’t replace the other. Anyone who has spent time on a plant floor knows there can be a big difference between what the ERP says and what’s actually happening. The system might show an order following the schedule, while the floor is dealing with the
following:
- A machine issue
- A quality problem
- Or a delay that hasn’t been recorded yet
That gap between what the system says and what’s really happening can quietly get expensive, and MES addresses it. ERP and MES get confused because both deal with manufacturing data, but they have different jobs.
ERP runs the business, MES runs the factory
The two work best together by connecting business planning with what’s actually happening on the shop floor. In this guide, we’ll break down the differences between ERP and MES, what each system does, and why manufacturers often need both.
What is ERP (Enterprise Resource Planning)?
For any business, ERP answers one core question: what do we need to make, when, with what materials, and at what cost?
ERP stands for Enterprise Resource Planning. It's the system that records business-side data of manufacturing: finance, procurement, inventory valuation, MRP, customer orders, and month-end close. If a question involves money, paper materials, or what's supposed to happen, ERP is usually where the answer lives.
To be precise, ERP supports the financial and planning space for any unit:
- General ledger and financial reporting
- Purchase orders and procurement
- Inventory valuation
- MRP (material requirements planning)
- Customer orders
- Month-end close
A Lookback on ERP Revolution
ERP evolved from MRP systems in the 1960s, became MRP II in the '80s, and matured into what we now call ERP in the '90s. The core idea was this: one database, one version of the truth, and every department reading the same numbers instead of separate spreadsheets.
Why is ERP not Enough to Manage Manufacturing Execution?
ERP unifies business data, even for a manufacturing production unit, but it lacks the real-time intelligence and advanced capabilities needed to manage manufacturing operations.
A manufacturing production floor needs advanced integration, real-time data collection, instant and event-based decision-making, and more. Let's see why ERP is not enough to run the shop floor:
Material Consumption is Not Tracked
ERP assumes material consumption exactly matches the bill of materials. It has no way to know about the dropped part, the substituted lot, or the rework that happened off the books.
No Real-Time Traceability
ERP has no visibility into why a product sits in "In Progress," whether the line is running normally, or whether it has been down for two hours. In ERP, traceability means knowing what you purchased, not which finished units that material ended up in.
Quality Comes at the End
ERP can log inspection plans and supplier scores just fine. It can't stop a line the instant a torque reading comes in out of spec. By the time a defect shows up in ERP, the part has usually already shipped.
No Update on Downtime
ERP can't tell you why and how a specific job took 8 hours to complete when the standard execution time was 6 hours. As a result, it affects the manufacturing KPI calculations and delivers an assumed OEE number.
ERP is excellent at what it was designed for: finances, materials, and plans moving across departments. ERP was never built to talk to a PLC or a barcode scanner.
What is MES (Manufacturing Execution System)?
MES is the core execution layer of manufacturing, responsible for controlling, monitoring, and managing process execution in real time. MES software connects people, machines, materials, and processes. In other words, MES takes the plan from ERP and helps turn it into actual production, working closer to the shop floor than ERP. In practice, MES is the system connected directly to the equipment. It pulls machine states, cycle times, and sensor data in real time instead of waiting for data updates.
A simple way to look at the manufacturing execution systems is:
- The Business Layer (ERP): What should we do this week, and do we have the materials and money to do it? What resources do we need?
- The Operations Layer (MES/MOM): How do we make it right now, and is it actually going well? What is happening during production?
- The Control Layer (SCADA/PLCs): What are the machines doing, and what motion should they make next? What is the equipment state right now?
- The Physical Layer: The actual equipment, sensors, and product.
MES sits between the business system and the equipment on the floor. It translates the plan into action, and it translates physical reality back into data the business can use. ERP cannot perform that translation. It doesn't speak the language of PLCs, barcode scanners, or torque wrenches.
ISA-95 defines this as a layered hierarchy, and it's the clearest way to see where each system actually lives:
| ISA-95 Level | System | Question it answers |
|---|---|---|
|
Level 4 (Business Planning & Logistics) |
ERP |
What should we make this week, and can we afford it? |
|
Level 3 (Manufacturing Operations Management) |
MES / MOM |
How do we make it right now, and is it going well? |
|
Level 2 (Supervisory Control) |
SCADA / HMI |
What are the machines doing, and how do we monitor them? |
|
Level 1 (Basic Control) |
PLCs / DCS |
What motion or action should equipment take next? |
|
Level 0 (Physical Process) |
Equipment, sensors, product |
— |
Key Functionalities and Benefits of MES
ERP can manage the production plan, but it usually doesn't handle detailed, real-time execution at each station. That is where MES adds value. Let's see what MES does that ERP cannot:
Real-Time Production Data
MES can capture machine states, cycle times, production counts, and process data in real time rather than relying on manual entries or end-of-shift updates.
Work Order Execution
ERP can release a work order, but MES helps manage it on the floor. It can show which job is running, what is next, where the order is in the process, and when it needs to be rerouted due to machine or production issues.
Digital Work Instructions
MES can provide operators with the exact steps, specifications, images, and other digital work instructions needed for a job. This reduces reliance on paper instructions and helps keep the process consistent.
Material Verification
MES verifies that the correct material, part, and lot are used at each step. A barcode scan can detect a wrong component early, preventing it from progressing further in production.
In-Process Quality
Quality checks can be performed directly at the workstation. If a measurement or process check fails, MES can either flag the issue or halt the process to prevent the problem from proceeding to the next operation.
Traceability and Genealogy
MES can create a detailed history of a product or batch: which materials were used, which machine produced it, who worked on it, which processes were followed, and what quality results were recorded.
Live OEE and Production Performance
Because MES works with actual production data, OEE and key production metrics are updated continuously rather than reconstructed later from manual reports.
MES vs ERP: What is the Difference Between MES and ERP?
MES and ERP are two important solutions for any manufacturing unit. ERP handles what should be built, when, and whether the budget and materials are there to support it. Whereas MES makes sure that the production plan is executed perfectly, part by part, minute by minute, on the shop floor.
Neither system is better, but both are built for different jobs, at different speeds, for different people. Friction starts when one is asked to do the other's job.
ERP Plans ---> MES Executes -------> Reports Back to ERP
Here's the side-by-side, for a quick reference:
| Category | ERP | MES |
|---|---|---|
|
Primary Focus |
What should we make, and can we afford it? |
What's happening on the floor right now, and is it correct? |
|
Time horizon |
Days, weeks, accounting periods |
Seconds, minutes, shift cycles |
|
Primary users |
Planners, buyers, finance, executives |
Operators, supervisors, quality technicians |
|
Data entry method |
Manual entry, batch uploads, reported completions |
Direct connection to PLCs, sensors, scanners, scales |
|
Update frequency |
Periodic: often daily or per transaction |
Continuous: updated as events happen |
|
Inventory view |
Financial valuation, on-hand quantity at a point in time |
Real-time WIP, material consumed at the point of use |
|
Traceability depth |
What was purchased, from which supplier, at what cost |
Which specific unit or serial number contains which lot |
|
Typical trigger |
Orders, invoices, purchase requisitions |
Machine faults, quality checks, dispatch events |
|
Quality management |
Stores inspection plans, supplier scorecards, NCRs after the fact |
Enforces in-process checks; can stop a line the moment a reading fails |
|
Scheduling |
High-level production plan, capacity at a macro level |
Minute-by-minute dispatch, re-sequencing when something breaks |
|
Labor tracking |
Standard hours, payroll-level reporting |
Actual time per operation, per operator, per station |
|
OEE / Performance data |
Calculated from standard hours and reported completions |
Calculated continuously from real machine states |
|
ISA-95 level |
Level 4 |
Level 3 |
|
Can it replace the other? |
No, has no way to see or control the floor in real time |
No, has no financial, procurement, or enterprise planning capability |
Let's understand the MES vs ERP differences in detail:
Scope of Operations
ERP covers the whole business side: every plant, every warehouse, and every department, rolled into one system. Whether you run three facilities or one, ERP consolidates all the data into a single view.
MES depends entirely on the platform. A legacy, on-premise MES is often deployed and licensed line by line. In contrast, a modern, cloud-based MES can easily aggregate live execution data from a single stamping line, from every line of a single plant, or from a dozen plants across different countries, all in one dashboard.
Data Granularity and Timing
ERP works with summarized data to answer direct questions like: "How did a product line perform last month?" and it'll give you a straight answer, because that's exactly the kind of question it was built to answer. But you can track on an ERP what happened on a specific line at a specific time.
MES is built for exactly that question: if a machine faults mid-shift, MES already has the fault code, the timestamp, and the operator on shift, because it was monitoring the equipment when it happened, not reconstructing the story afterward.
Who Actually Uses Each System
ERP's daily users are planners: buyers, finance staff, and executives; people making decisions about budgets, orders, and capacity.
MES's daily users are the people physically on the floor: operators, shift supervisors, and quality technicians. An operator scanning a barcode before loading a part, or a supervisor checking a dashboard to see which station is falling behind, is what MES use looks like, shift after shift.
System Integrations
ERP integrates outward with other business software: CRM, HR, e-commerce platforms, and EDI with customers and suppliers. Its job is to keep the business side of the company in sync.
MES integrates inward, toward the equipment itself: PLCs, sensors, barcode scanners, torque wrenches, and scales. Its job is to keep the physical side of production in sync, which is a fundamentally different integration problem and usually why MES rollouts take longer to plan than people expect.
Traceability Depth
ERP's traceability stops at the purchase order: which supplier, which lot, at what cost, and received on what date. That's useful for procurement and basic compliance, but it's a purchasing record, not a production record.
MES traceability goes much deeper than ERP traceability. It can identify the exact serial number or unit that contains material from a specific lot, show which machine produced it, and record the quality gate where it was checked.
Quality Management
ERP's approach to quality management mostly involves paperwork, such as inspection plans, supplier scorecards, and non-conformance reports filed after issues have occurred. In contrast, MES's approach is real-time; if a torque reading is out of specification, MES can halt the production line immediately, preventing further parts from being produced, instead of just recording the problem for review later.
Scheduling
ERP produces the master schedule: what should run, on which line, and by which date, based on demand forecasts and overall capacity. It's planning at the level of a week or a month.
MES (or the scheduling layer inside a MOM platform) takes that plan and determines the next twenty minutes on the actual floor, re-sequencing jobs the moment a machine goes down or an operator calls in sick, something ERP has no mechanism to do in real time.
Labor and Cost Tracking
ERP tracks labor at the level finance needs it: standard hours per unit, cost roll-ups, and payroll reporting. It's accurate in aggregate over a pay period.
MES tracks labor at the level the floor needs: which operator ran which operation for how long, compared to the standard- data granular enough to spot a training gap or a bottleneck at a single station, not just a department-wide average.
Get a closer look at how MES connects production, machines, materials, quality, and people in real time.
How Does ERP Create a Manufacturing Gap?
When we talk about the gap between ERP and the shop floor, it is about the space between what a system assumes happened and what actually happened, and how long it takes for reality to catch up with the record.
It shows up in a few consistent ways:
- A production gap: ERP records status as "in progress" or "complete," while the floor experienced a specific fault, a specific delay, or a specific substitution that never gets captured at that level of detail.
- An ownership gap: N obody is clearly responsible for reconciling the ERP number against the floor number, so it defaults to a person doing it manually, usually right before a meeting.
ERP and MES Integration: How They Work Alongside
The discrepancy isn't a fault in either system alone. ERP functions as intended, and so does MES. The gap occurs because, without a deliberate linkage, they cannot stay synchronized. This is an integration issue, not a software flaw, and it can be fixed.
In a properly integrated setup, information moves in both directions:
ERP → MES: Work orders, bills of materials, routings, production schedules, and master data flow down to the floor.
This tells MES what is supposed to happen.
MES → ERP: Actual production quantities, real material consumption, scrap and rework, actual labor hours, quality results, and downtime analysis data flow back up.
This tells ERP what really happened, so it's costing, inventory, and reporting to reflect reality instead of assumption.
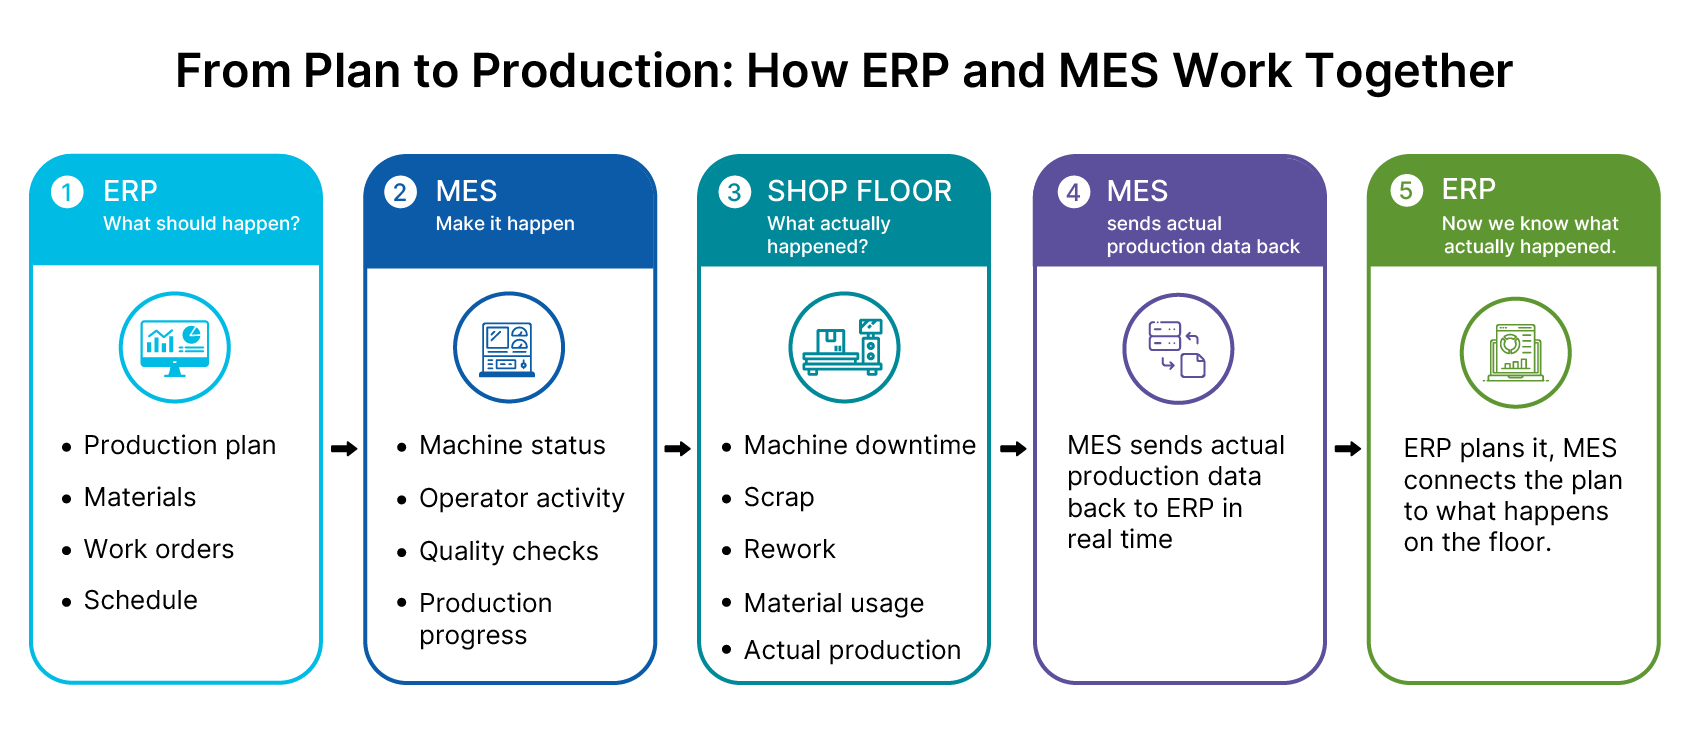
Data Transmission Between MES & ERP
The formal standard governing this exchange is ISA-95 / B2MML, which defines a common data model, so ERP and MES (or a broader MOM platform) can exchange information without a custom-built translation layer for every plant. In practice, this occurs through native connectors or APIs, ideally configured once and left to run, rather through a manually updated spreadsheet.
Benefits of MES & ERP Integration
- Inventory: Stays accurate because MES reports actual consumption back to ERP instead of ERP guessing from the BOM.
- Quality: Stays connected because in-process results from MES automatically feed ERP's supplier scorecards and NCR records.
- Scheduling: Stays realistic because ERP's master schedule is continuously informed by what MES reports is achievable on the floor that shift.
- Labor: Reconciles because MES's actual time-per-operation data flows into ERP's payroll and costing without manual re-entry.
MES vs ERP: The Difference in Practice
Imagine ERP shows that an order is on schedule. MES can show a very different picture: the machine has been down for 30 minutes, production is running below the expected rate, and the latest quality check has failed.
That is the gap MES is designed to close.
ERP tells you what was planned, and MES shows you what is happening on the floor and helps your team act on it. For simple manufacturing operations, ERP may be enough. But when you need real-time machine data, tighter process control, in-process quality, detailed traceability, or live production performance, MES provides the shop-floor visibility and execution that ERP alone typically cannot.
The gap between your ERP and your shop floor isn't going to close on its own
Every month it stays open, you're building product on incomplete data and finding out about problems later than you should.
If you want a second opinion on where the gap actually is in your operation, we're happy to walk through it with you: no generic demo, just a look at your current setup and an honest read on whether MOM makes sense for you right now or not yet.
ERP manages business planning and enterprise-wide processes, including finance, procurement, inventory, customer orders, and material requirements. MES manages real-time production execution on the shop floor by connecting operators, machines, materials, quality checks, and work orders.
No. MES does not provide the financial management, procurement, customer order processing, or enterprise planning capabilities of ERP. The two systems are complementary: ERP runs the business, while MES helps run and monitor factory operations.
ERP typically relies on manual entries, reported completions, or periodic data updates. This can create a delay between what is happening in production and what appears in the system. MES closes this visibility gap by capturing machine states, production counts, quality results, downtime, and material consumption in real time.
ERP sends production plans, work orders, bills of materials, routings, schedules, and master data to MES. MES then returns actual production quantities, material usage, labor hours, scrap, rework, downtime, and quality results. This two-way exchange keeps planning, inventory, costing, and production data aligned.
A manufacturer may need MES when it requires real-time production monitoring, detailed product traceability, in-process quality control, live OEE reporting, digital work instructions, or direct equipment connectivity. MES becomes especially valuable when paper records, spreadsheets, and delayed ERP updates no longer provide sufficient visibility or control.